On this page
In manufacturing, the straightness of material affects both how parts function and how safely they run. Straightening machines reduce bends, curvature, and warp in metal bar, rod, tube, and wire so the material meets a specified straightness tolerance before the next production step. Residual curvature can be reduced but not eliminated. The tolerance that is practical depends on the material, its diameter, how curved it is on arrival, and the machine setup.
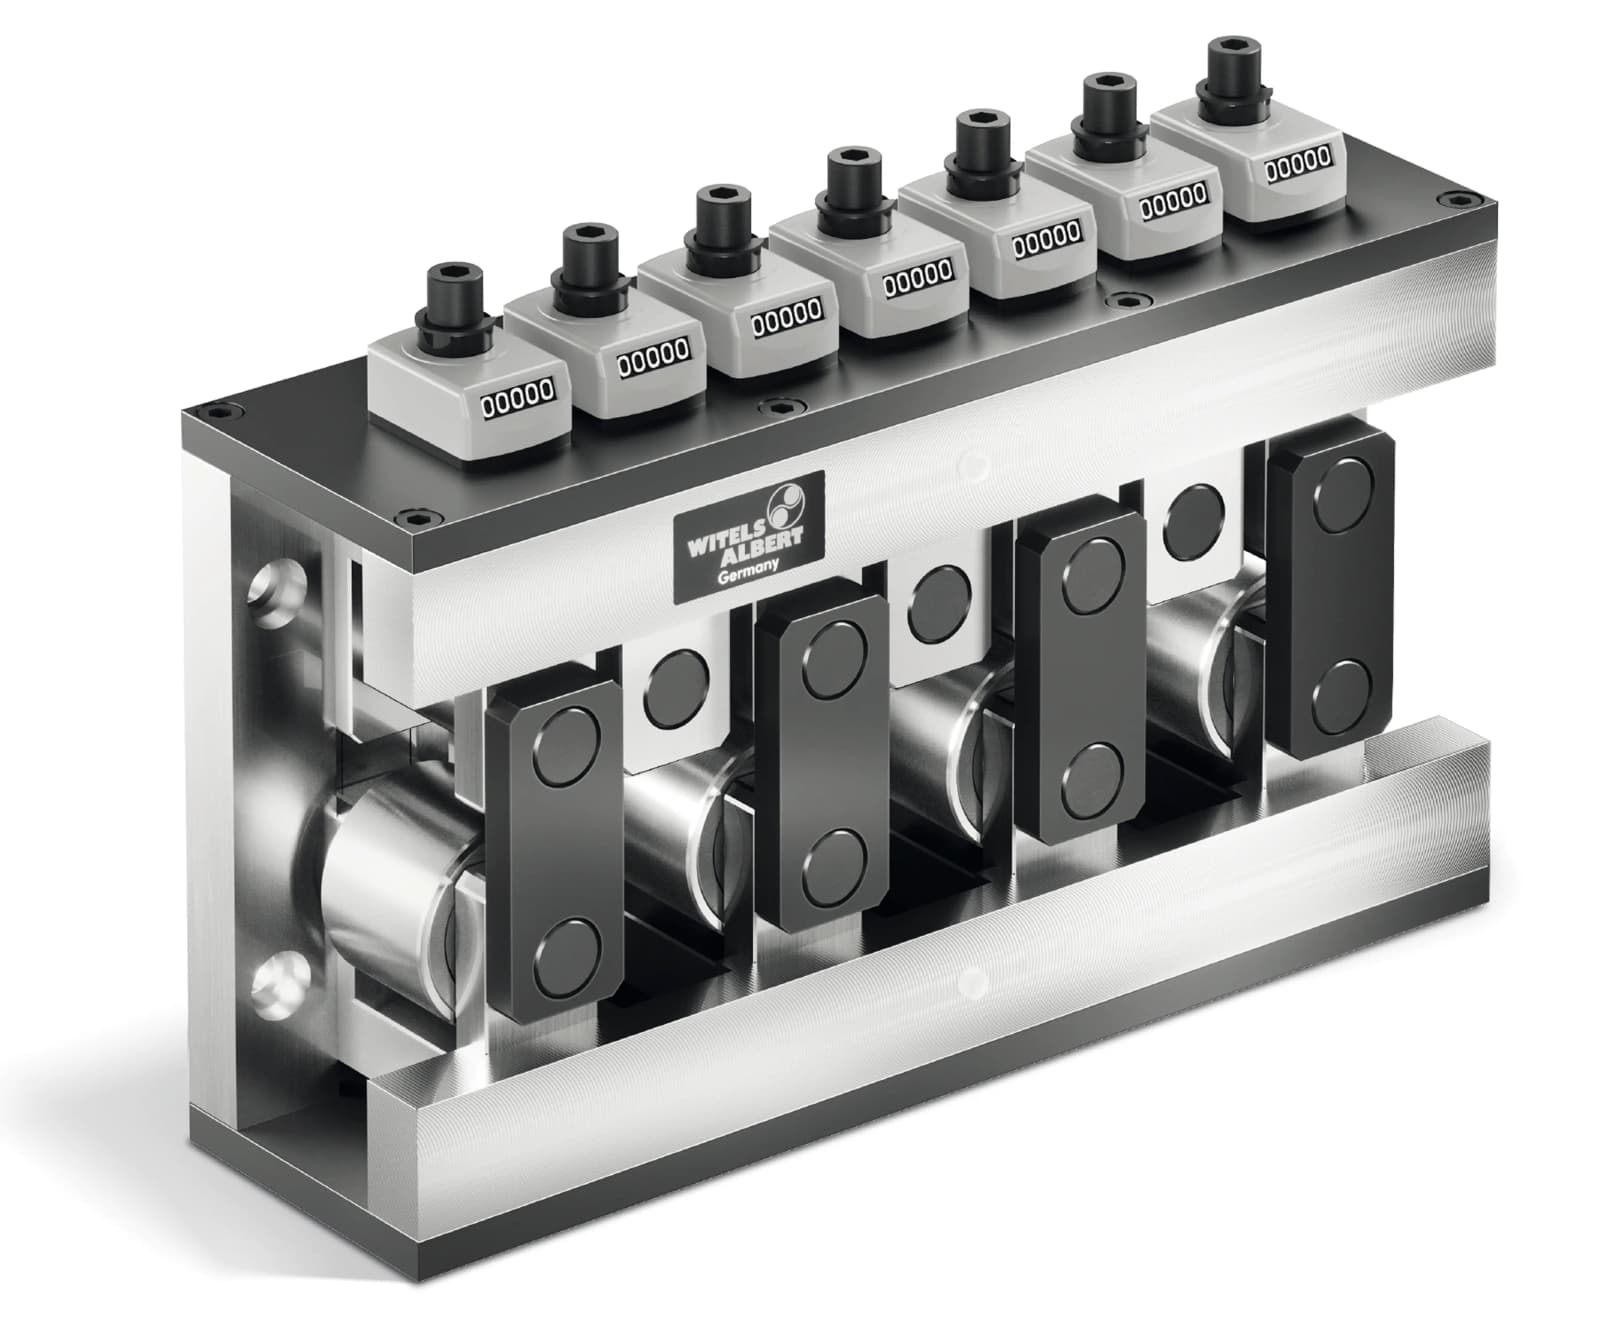
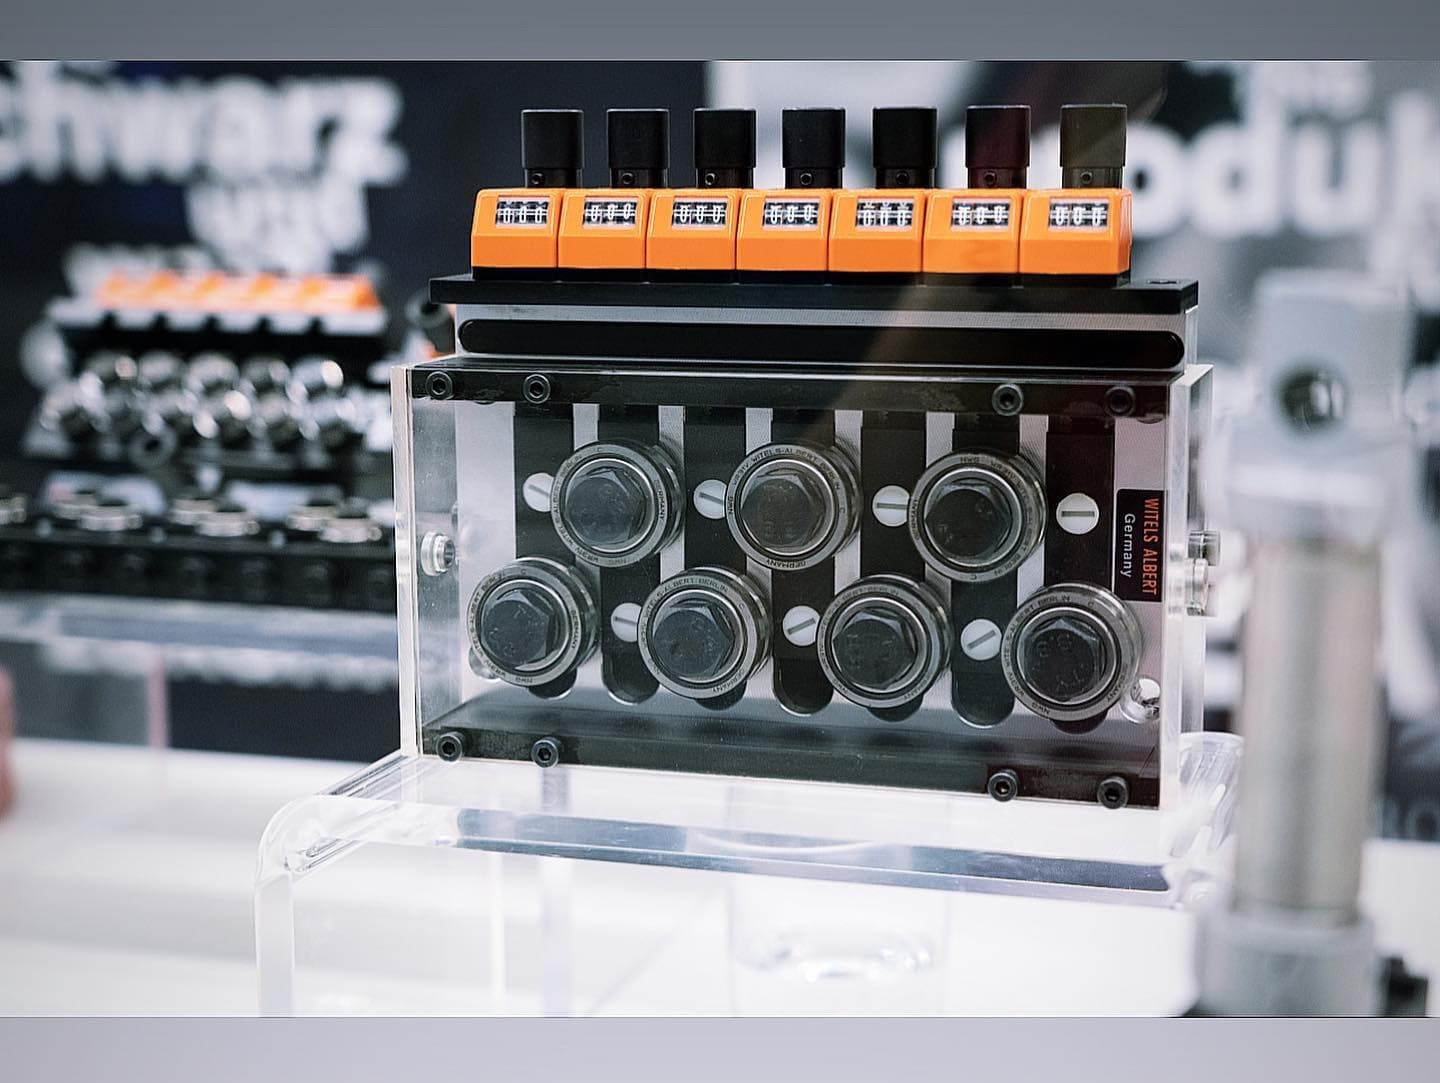
A roll straightening machine passes the material through two offset rows of rolls. The rolls bend it back and forth in alternating directions, with the bends getting smaller toward the exit. The first bends are large enough to yield the material permanently, which resets most of the curvature it arrived with. The later, smaller bends refine what is left. No material is cut or removed.
How Do Straightening Machines Work?
Roll straighteners work by alternating bending. The material runs through two offset rows of rolls and is bent over each roll in turn, first one way, then the other.
Plastic deformation beyond yield. To change the shape of metal permanently, the bend has to take the outer fibers of the cross-section past the material's yield strength. Bending that stays elastic only springs back to the original curvature. The first rolls therefore apply the largest bends, large enough to yield the material and overwrite the curvature it arrived with.
Decreasing bends. Each following roll applies a smaller bend, so the remaining variation in curvature shrinks roll by roll. The last rolls apply very little bending and mainly guide the material out in a line.
Springback. When the material leaves a roll, the elastic part of the bend recovers. The higher a material's yield strength relative to its stiffness (modulus of elasticity), the more it springs back, so the machine has to bend it further to end up with the intended shape.
Residual curvature. What remains after the last roll is the residual curvature. It can be made small but not zero. Springback, variation along the length of the material, and residual stress mean the result is a tolerance, not a perfect line.
What roll count, pitch, and infeed change:
- Roll count. More rolls give more alternating bends and a gentler step-down in bend size. That generally lowers and evens out the residual curvature and tolerates more variation in the incoming material. More rolls also mean a longer machine, more contact points, and more places to mark the surface, so roll count is a trade-off, not a quality score.
- Roll pitch and roll size. Pitch (the spacing between rolls) has to match the diameter of the material. The curvature needed to yield the outer fibers is roughly proportional to yield strength divided by (modulus × diameter). Thick material yields at a gentler curvature but needs much higher bending loads, so it takes a larger pitch and larger rolls. Fine wire, and high-yield-strength material of a given size, need a tighter bend, so a smaller pitch or more infeed. This is why each straightener series is specified for a stated size range.
- Infeed (roll offset). Infeed sets how far the rolls overlap, and so how much bend is applied. Too little leaves the material only partly yielded and residual curvature remains. Too much overbends it, adds wear and surface marking, and can leave curvature in the opposite direction. Infeed is adjusted for each material, diameter, and lot.
Typical roll straightener features:
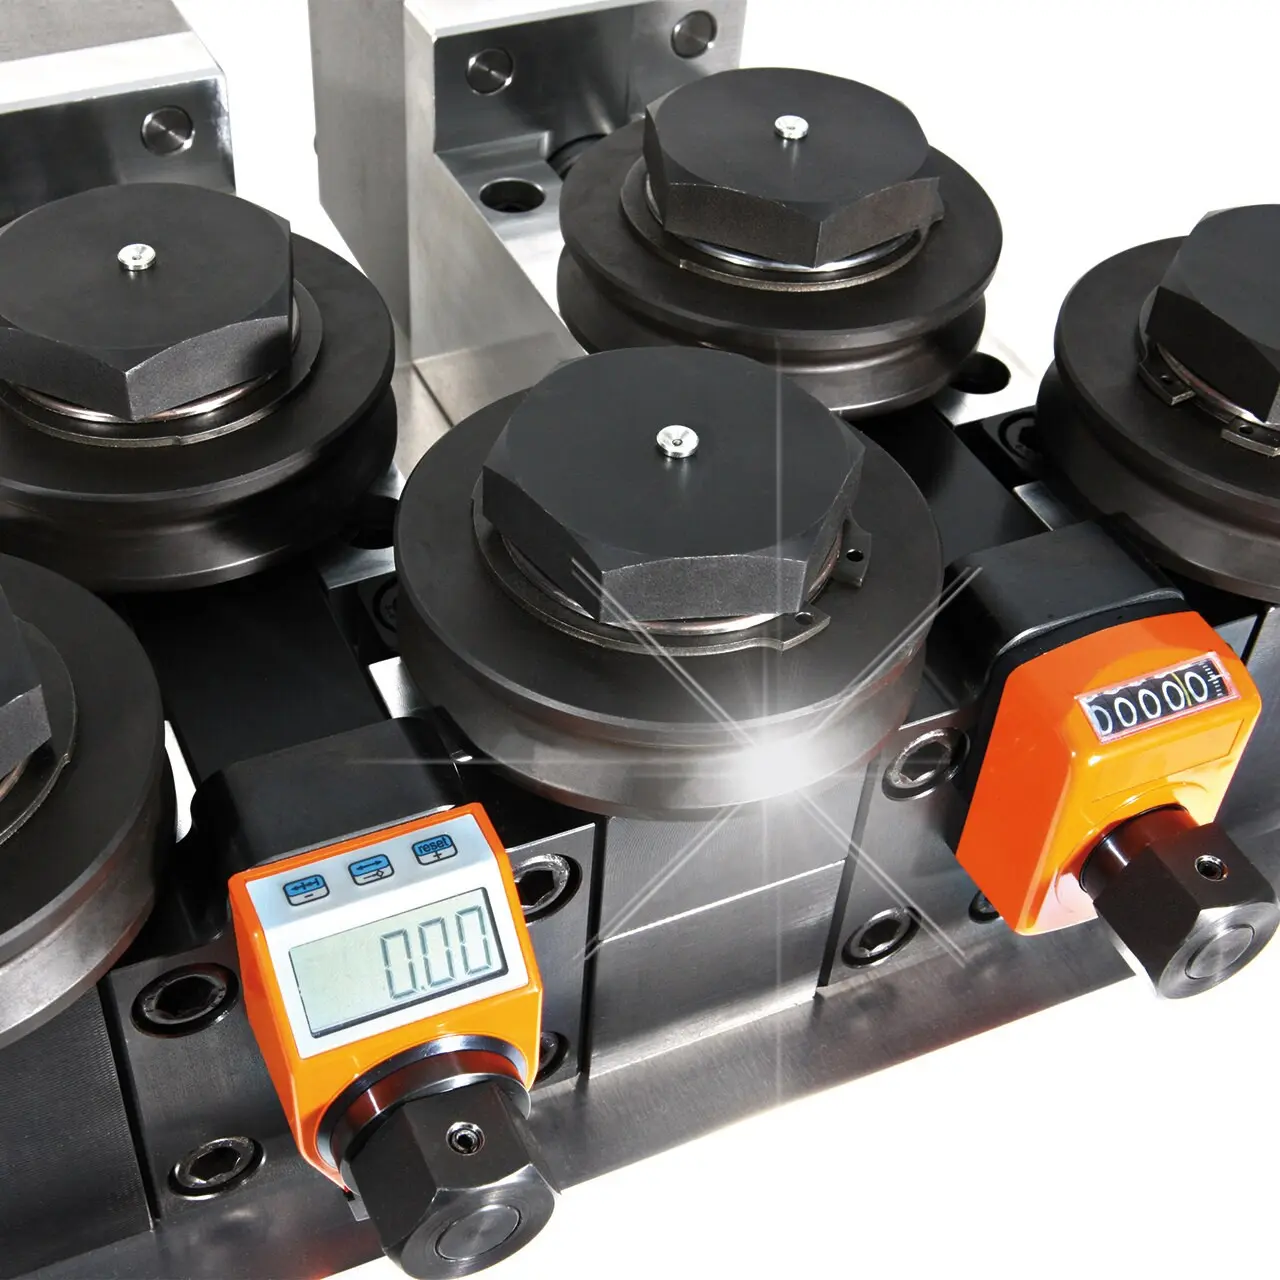
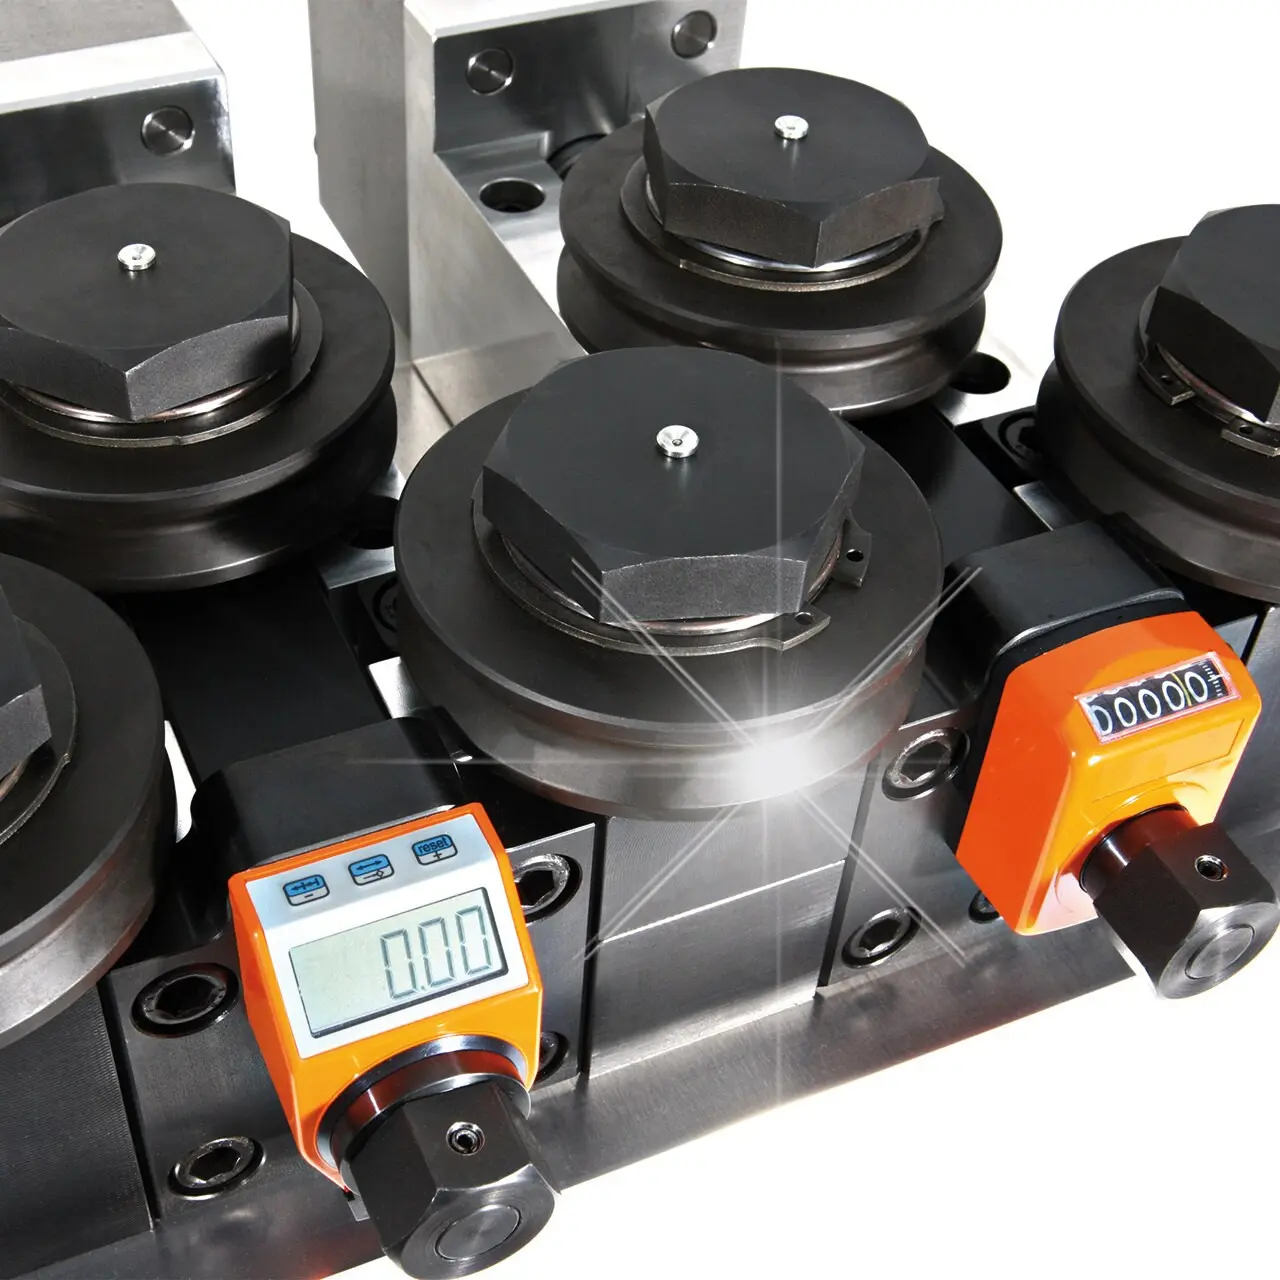
Adjustable roll position (infeed). Each adjustable roll is set by an adjusting screw, usually with a scale, so the bend at that roll can be set and repeated.
Material transport. In-line wire straighteners usually have free-running rolls, and a drive unit, capstan, or the line pulls or feeds the material through at line speed. Some rotary, bar, and tube straighteners drive the material or rotate the tooling.
Line integration. Straighteners are commonly installed in-line ahead of cut-to-length, forming, or feeding equipment. The interface requirements are set by the line.
Repeatable settings. Scales or indicators on the roll adjustments let operators return to a recorded setup. Results still depend on lot-to-lot variation in the material.
Limits of Roll Straightening
- Residual curvature is reduced, not eliminated. A straightness requirement should state the tolerance, the measuring length, and the measuring method.
- Hard and large material is harder to straighten. High-yield-strength material springs back more, needs a tighter bend for its size to yield, and needs higher bending loads, so it typically calls for more infeed, often more rolls, and a machine rated for those loads. Large-diameter material needs larger rolls and a larger pitch. For some combinations, the required tolerance may be out of reach for a given machine.
- Cast and helix need two planes. A single-plane unit corrects curvature in one plane only. Coiled wire is usually straightened with a second set of rolls rotated 90 degrees, or with a rotary straightener.
- Surface marking. The rolls press on the material. Soft metals, coated wire, and thin-wall tube can mark or flatten. Roll material, groove profile, pitch, and infeed are chosen to limit this, but some marking risk remains.
- The material changes. Straightening cold-works the surface layers and changes residual stress. A cut length can bow slightly after cutting if residual stress releases.
- Some defects cannot be fixed. Kinks, local damage, and twist are not corrected by a roll straightener.
Why Use a Straightening Machine?
Straightening machines offer several key benefits:
Better fit and consistency. Straighter material locates more accurately in dies, guides, and fixtures and fits mating parts more consistently. Straightening corrects geometry only. It does not add strength, and the cold working involved can change the material's surface condition and residual stress.
Less manual rework. In-line straightening replaces a separate manual or offline straightening step, and straighter input feeds more steadily into downstream equipment.
Lower scrap and rework. Reducing curvature-related rejects can lower scrap and rework. The saving depends on the application and on how much of the current scrap is caused by bent material.
Wide material range. Roll straightening is used on steel, aluminum, copper, and other metals in round, flat, profile, and tube form. Each machine covers a defined size range and cross-section, and soft metals and hollow sections need roll grooves and settings that limit marking and ovality.
More consistent downstream processes. Straighter input gives cutting, welding, forming, and measuring operations a more consistent starting geometry, which makes accurate results easier to hold.
Key Material Properties in Straightening
These material properties decide how metal responds to the bending in a straightener:
Yield strength. This is the stress at which a material starts to deform permanently. Roll straightening works by bending the material past this point. A higher yield strength means higher bending loads and more springback, so the machine needs more bending, and often more rolls, to reach the same residual curvature.
Ductility and strain limits. Straightening needs the outer fibers of the material to go past yield, and the metal has to tolerate that strain. The limits are ductility (how much strain it takes before cracking), work hardening, and surface sensitivity. Straightening past what the material can tolerate, or with rolls too small for the diameter, causes cracking, excess cold work, marking, or ovality in tube.
Modulus of elasticity. This is a measure of stiffness, how much a material deflects elastically under load. In straightening it affects springback. For the same yield strength, a material with a lower modulus recovers more of the bend after each roll, so it needs more overbend to end up in the same place.
Work hardening. Each yielding bend cold-works the material. This can raise surface hardness and change the residual stress state, which matters for springs, parts with tight tolerances after cutting, and any application that depends on the material's delivered temper.
Alignment and Roll Planes
Two things must be right for the rolls to correct the curvature: the plane the rolls bend in, and how well the material is guided into the rolls. A single-plane straightener corrects curvature in the plane of its rolls only, so the roll plane has to match the plane of the curvature. Wire from coils usually has curvature in more than one plane (cast and helix) and is straightened in two planes, with a second set of rolls rotated 90 degrees to the first, or with a rotary straightener. Entry and exit guides keep the material centered in the roll grooves. If the material is not properly aligned with the machine’s rollers or dies, several issues can arise:
Uneven bending. Misalignment between the guides and the rolls bends one side of the material more than the other. That can overbend low-ductility material, mark the surface, and leave curvature in one plane uncorrected.
Inconsistent straightening. If the material is not aligned properly, some sections come out straighter than others, and parts that are meant to fit together may not line up.
Uneven roll wear. A misaligned system wears the rolls and guides unevenly, which shortens their service life and means more frequent maintenance.
New bends and twists. Material forced through misaligned rolls or guides can pick up new bends or twists. This can reduce or cancel the benefit of straightening and lead to rework.
Safety. Material that is not guided properly can whip or exit off-axis, which is a hazard for operators.
The material should be fed in the plane and position the rolls are set for. Adjustable entry and exit guides help hold the material in line with the rolls. Some lines add measurement or sensing downstream of the straightener to check the result.
Where Are Straightening Machines Used?
Straightening machines are used in a wide variety of industries:
Automotive. Shafts, rods, and tube for steering, suspension, and fluid lines are held to a straightness tolerance on the part drawing so they run true, assemble correctly, and feed reliably into forming and machining.
Aerospace. Tube and rod stock is often specified to a tight straightness tolerance before machining, bending, or welding. Material grade and temper determine the springback to expect and how the machine is set up, and the applicable specification governs inspection.
Construction products. Wire and rod used in mesh, fencing, and fasteners are straightened before cutting, welding, or forming. Structural sections and rebar are usually handled by other machine types, such as presses or straighten-and-cut machines, which are outside the in-line roll straighteners described here.
Furniture. Metal frames for tables and chairs are straightened before bending or welding. Tube needs roll grooves and settings that limit marking and ovality, because the frame is usually visible.
Industrial equipment. Shafts and rods are straightened to limit runout, vibration, and uneven wear in service. Straightening also changes residual stress, so critical parts should be specified and verified against the part drawing.
Tube and pipe. Straight tube fits more consistently into fixtures and weld joints, which helps fit-up. Leak-tightness depends on the weld, not on straightness alone. In tube, the main limits are ovality, wall flattening, and roll marking, which roll pitch, groove profile, and infeed are chosen to control.
Matching the roll plane, roll count, pitch, and infeed to the material's yield strength, diameter, and incoming curvature gives the lowest practical residual curvature for that material. It does not remove the need to specify a straightness tolerance and a way to measure it.
Choosing a Configuration
To select a straightener, have these ready: material and yield strength, diameter or cross-section range, how curved the incoming material is (including cast and helix), the residual curvature you need and how you measure it, line speed, and how sensitive the surface is. The more of this you share, the closer the recommendation. The Willy Wire questionnaire collects these details for wire.
Written by WITELS-ALBERT Engineering Team
Practical guidance from the straightening technology specialists who design and support precision wire, tube, strip, cable, and profile straightening solutions.
Frequently asked questions
What is a straightening machine?
A straightening machine reduces bends, curvature, and warp in metal bar, rod, tube, strip, or wire. In a roll straightener, the material passes through two offset rows of rolls that bend it back and forth with decreasing amplitude. The first bends yield the material and reset its curvature, and the later bends refine it. Residual curvature is reduced, not eliminated, and no metal is cut or removed.
How does a wire straightener work?
A wire straightener passes wire through offset rolls that bend it alternately in opposite directions, with the largest bends at the entry. These bends take the wire past its yield strength, so its original curvature is overwritten. Smaller bends follow, and the wire springs back slightly as it leaves each roll. The rolls are set by roll position (infeed), not by applied pressure.
What does a straightener do?
A straightener reduces bends, curves, and warp so material is straighter for cutting, forming, welding, or coating. It bends the material past its yield strength in a controlled sequence, then lets it spring back. The material is permanently deformed by design. How straight it becomes depends on its yield strength, diameter, incoming curvature, roll count, roll pitch, and infeed.
How do you straighten wire?
Feed the wire through a straightener whose roll plane matches the plane of its curvature. Offset rolls bend it back and forth with decreasing amplitude, and the infeed at each roll sets the bend. Wire from coils usually has cast and helix, which need two planes of rolls. Correct alignment and entry guidance keep the wire centered in the rolls and prevent uneven wear and new bends.
What types of straightening machines are there?
Roll-type machines use straightening rolls in two parallel, mutually offset rows that bend material back and forth as it passes through. Rotary straightening spins the material or the tooling to correct curvature in all planes, and is used for bar, rod, tube, and wire. Stretch-bend straightening combines bending around small rolls with tensile stress. The right type depends on the material, cross-section, and required straightness.
Why is proper alignment important when straightening?
The roll planes must match the plane of the material's curvature, and the entry and exit guides must hold the material centered in the rolls. Misalignment can leave curvature uncorrected in one plane, cause uneven roll wear and surface scratches, and put new bends into the material. It can also let material whip or exit off-axis, which is a hazard for operators.
What is the difference between a straightener and a straightening machine?
A straightening machine has elements for both transporting and straightening the material, for example driven rolls. A straightener has only straightening elements: its rolls are not driven, so drive units, pull-in units or the line itself move the material through it. A straightener can therefore be used inside a straightening machine.
How many rolls does a straightening machine need?
More rolls give more alternating bends and a gentler step-down in bend size, which generally lowers and evens out residual curvature and tolerates more variation in the incoming material. More rolls also mean a longer machine, more contact points and more places to mark the surface, so roll count is a trade-off, not a quality score.
Is a roll straightener the same as a straighten-and-cut machine?
No. A roll straightener reduces curvature in wire, tube, strip, cable or profile as it runs through offset rolls on a continuous line. A straighten-and-cut machine straightens rebar or rod and cuts it to length in one machine, a different process category.